Customer Case
The choice of tens of thousands+customers.
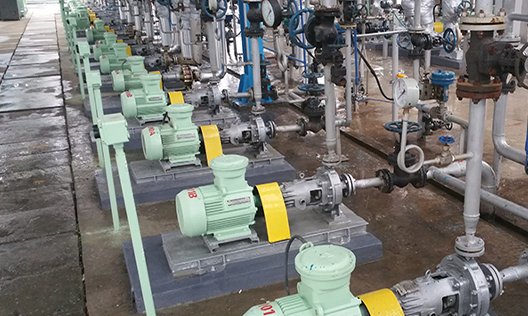
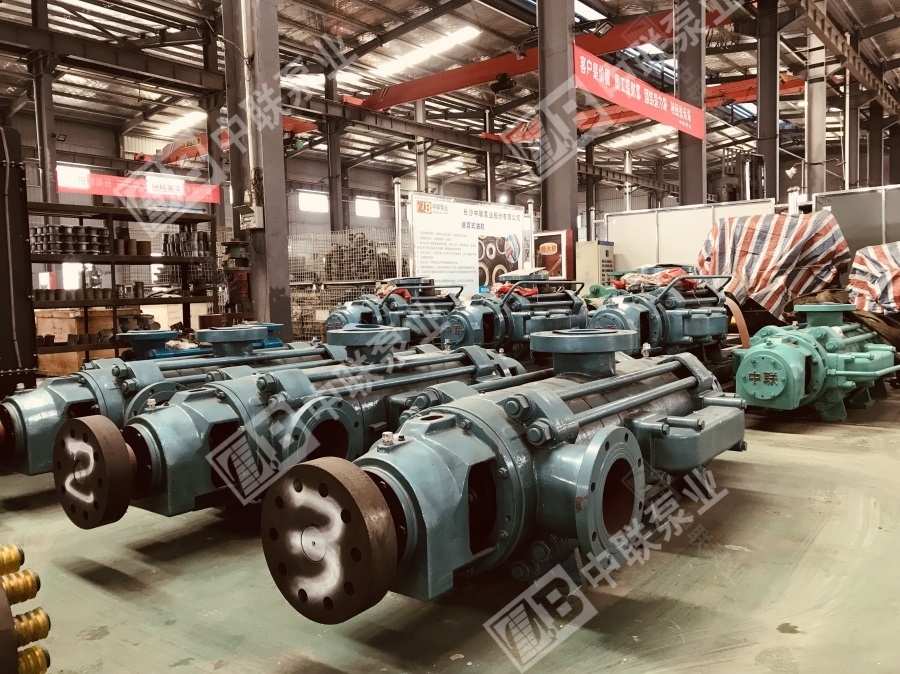
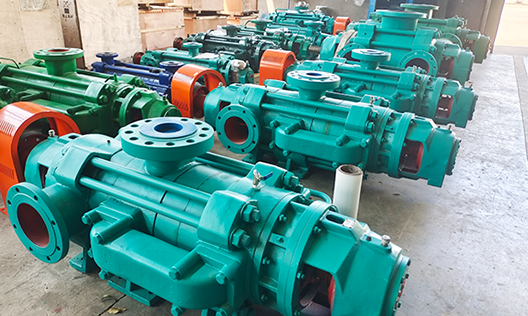
The Heilonggou Coal Mine, after undergoing a safety assessment, was identified as a mine with risks of gas outbursts and potential coal dust explosion hazards. Consequently, stringent requirements have been set forth regarding the safety performance, explosion-proof ratings, and reliability of underground equipment. On August 26, 2014, Changsha Zhonglian Pump Industry Co., Ltd. successfully won the bid for the mine’s main drainage equipment procurement project, providing the mine with both the primary drainage units and their accompanying auxiliary machinery. Notably, the core underground drainage equipment selected for this project is the MDP-type mining self-balancing multistage centrifugal pump. This pump model employs a bottom-valve-free drainage system, which effectively simplifies the overall structure of the drainage system, reduces potential failure points, and enhances both drainage efficiency and operational stability. Below are the technical specifications and equipment details provided by Changsha Zhonglian Pump Industry specifically tailored for the mine’s main drainage system.
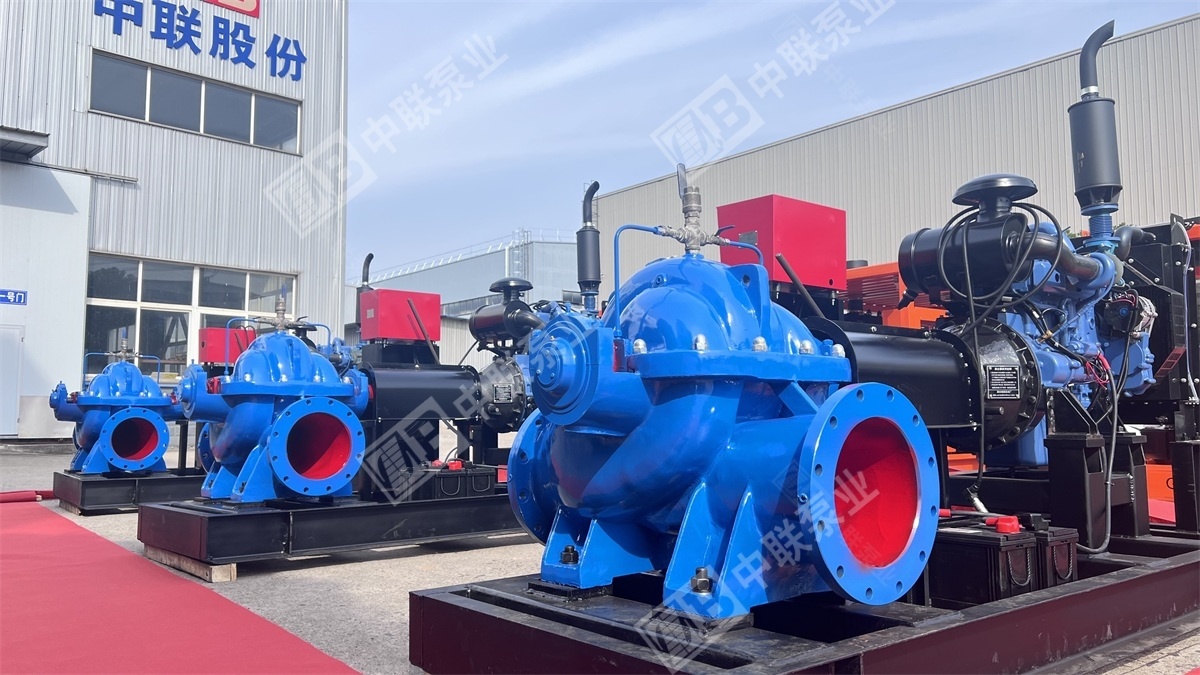
On this sunny and vibrant day, the warehouse was bustling with activity as Zhonglian Pump Industry's international trade team carefully loaded a batch of single-stage centrifugal pump units—diesel-powered engines—destined for Saudi Arabia. Not only are these units visually stunning, but they also boast exceptional performance. Looking back at this deal, from the initial contact to the final agreement, it took two months to complete. Though the process was marked by a few challenges along the way, the end result has been truly rewarding.
Changsha Zhonglian Pump Industry successfully participated in the construction of a steelmaking continuous casting project powered by an electric furnace in Tanzania, providing the country's steel industry company with specialized pump units and technical support essential for the plant's large-scale blast furnace's closed-loop desalinated water system, as well as its clean and turbid circulating water systems. This collaboration not only showcased Zhonglian Pump Industry's technological expertise but also earned the company greater recognition in the international market.
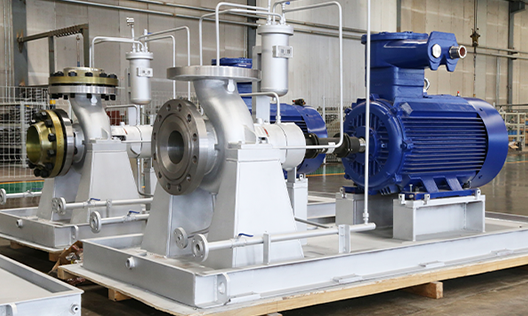
A trading company based in Shenzhen has established a solid business presence in the Malaysian market for quite some time. Leveraging its extensive experience and strong reputation, it successfully secured a supply agreement with the project owner for boiler feedwater pumps. Following this, the customer reached out to us at Changsha Zoomlion Pump Industry, seeking high-quality solutions for boiler feedwater pumps.
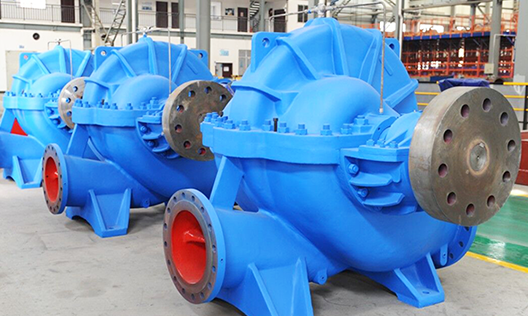
Due to business expansion needs, a shipping company in Dalian has recently launched a new sand-dredging operation and plans to purchase three sand-dredging pumps. While searching online for a suitable manufacturer, they reached out to the Sales Department of Changsha Zoomlion Pump Industry. After thorough technical discussions and gaining a deep understanding of our products, the customer ultimately chose our company’s GS-type, high-efficiency, horizontal split-case, double-suction centrifugal pump.
Customer Requirements and Technical Communication: When looking for sand-dredging pumps, the Dalian Shipping Company provided detailed specifications regarding material selection and operational specifics.
[Good News] We warmly congratulate a certain heating company on choosing Changsha Zoomlion Pump Industry for its district heating network project’s cooling water pump procurement! After six months of meticulous effort—spanning multiple rounds of information gathering, on-site inspections, and technical solution evaluations—the company has finalized its decision to equip the project with our company’s high-efficiency GS-type horizontal double-suction centrifugal pumps.
Warmest congratulations to a certain environmental engineering company in Luoyang for purchasing the D200-50*8 multi-stage centrifugal pump from Changsha Zhonglian Pump Industry! During July's outstanding sales performance, the Luoyang-based company reached out to us online, seeking a clear-water pump capable of meeting their 400-meter head requirement. After thorough discussions and expert selection assistance, the customer ultimately chose our company’s D200-50*8 multi-stage centrifugal pump—and promptly placed an order for two units, earmarked for their cutting-edge environmental protection project.