-
Products
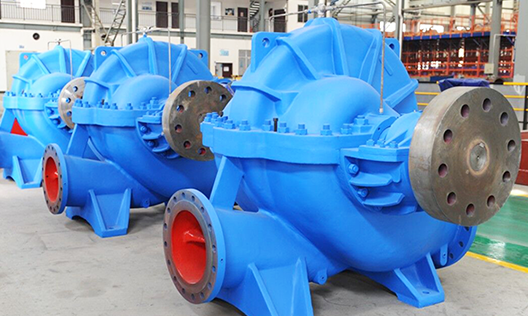
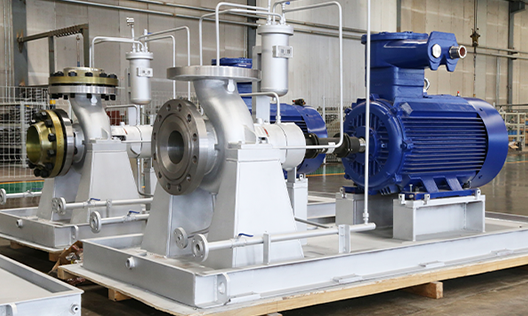
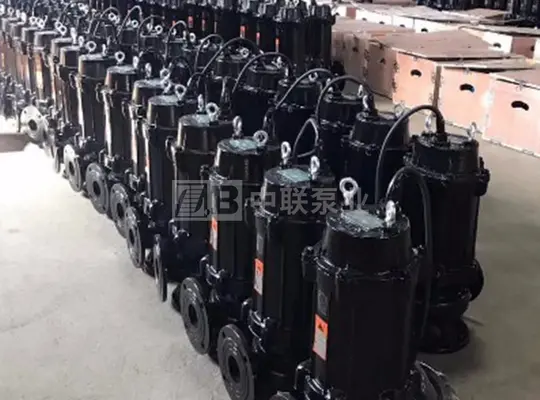
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Understanding Condensate Pumps: Essential Components for Efficient Industrial Operations
Publication Date:
2026-08-24
Author:
Source:


At their core, condensate pumps work by collecting condensate in a reservoir or sump and then automatically pumping it away to a designated discharge point. This is particularly important in systems like HVAC (heating, ventilation, and air conditioning), where condensate can build up rapidly. By removing this excess water, condensate pumps help maintain a dry environment, enhancing the performance of heating and cooling systems and preventing potential failures.
One of the significant advantages of condensate pumps is their ability to operate automatically, often triggered by float switches that detect rising water levels. This automation not only reduces the need for manual intervention but also helps optimize efficiency by ensuring that condensate is removed as soon as it accumulates. Additionally, many modern condensate pumps are designed with energy efficiency in mind, allowing for reduced operational costs over time.
The applications of condensate pumps extend beyond HVAC systems. They are also employed in various industrial processes involving steam generation, refrigeration, and other applications that produce condensate. In manufacturing facilities, for instance, condensate pumps play a crucial role in ensuring that machinery operates smoothly without the disruptive effects of water accumulation. This reliability is essential for maintaining production schedules and avoiding costly downtime.
When selecting a condensate pump for industrial use, several factors should be considered, including the pump's capacity, lift height, and compatibility with the specific system in which it will be installed. Understanding the unique requirements of the application will aid in choosing the right pump that can handle varying volumes of condensate effectively.
In summary, condensate pumps are indispensable components in industrial operations, ensuring that condensate is efficiently managed to prevent system failures and enhance overall operational efficiency. By understanding their functionality, applications, and selection criteria, professionals can make informed decisions that contribute to the longevity and reliability of their industrial equipment. Emphasizing the importance of these pumps can lead to more efficient processes and improved productivity in the long run.
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha