-
Products
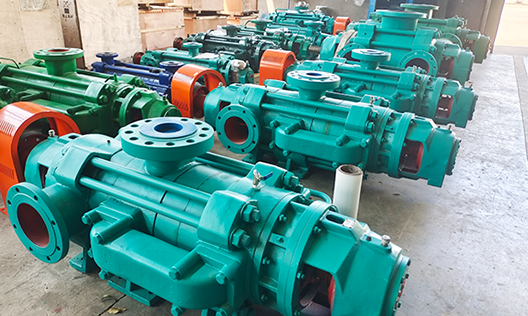
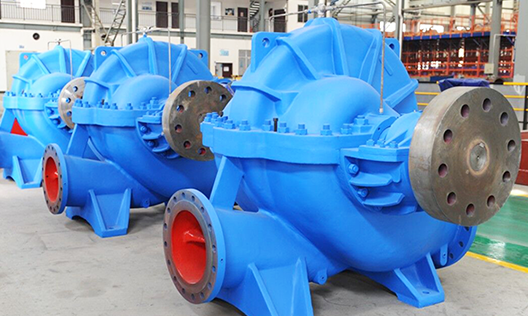
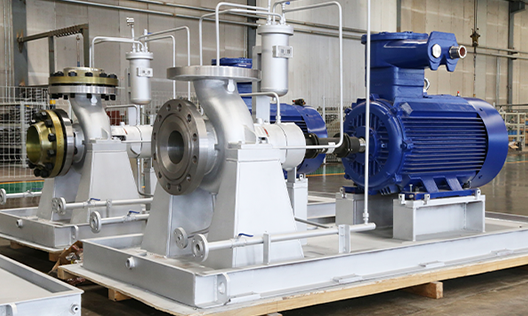
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
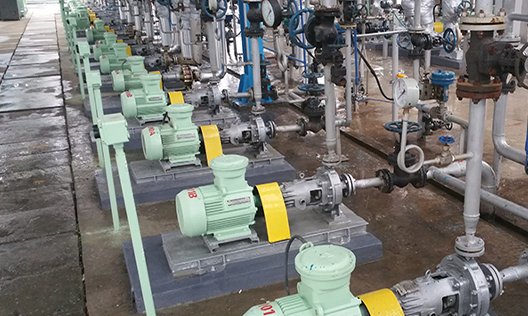
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Essential Insights into Quality Submersible Pumps for Industrial Applications
Publication Date:
2026-05-08
Author:
Source:


One of the primary characteristics to consider in a quality submersible pump is its construction material. Pumps made from high-grade stainless steel or thermoplastic materials are less susceptible to corrosion and wear, ensuring longevity even in harsh environments. This durability is crucial, especially in industries where pumps are exposed to abrasive or chemically aggressive fluids.
Efficiency is another vital factor. A quality submersible pump should have a high hydraulic efficiency, which translates to better performance with lower energy consumption. This not only reduces operational costs but also minimizes the environmental impact of your industrial processes. Look for pumps that feature advanced hydraulic designs, which optimize flow rates and pressure outputs while maintaining energy efficiency.
Maintenance is an aspect that should not be overlooked when selecting a quality submersible pump. Regular inspection and servicing can prevent unexpected failures and extend the lifespan of the equipment. It is advisable to choose pumps that are designed for ease of maintenance, allowing for quick and hassle-free servicing. This includes features like removable components and accessible motor assemblies, which simplify routine checks and repairs.
In addition to these features, consider the pump's specific application capabilities. Quality submersible pumps vary in design and functionality based on their intended use. For instance, some pumps are specifically engineered for handling solids, while others excel at managing clean water. Understanding your specific requirements will guide you in selecting a pump that not only meets but exceeds your operational needs.
Lastly, it is important to evaluate the manufacturer’s reputation and customer support. A reliable manufacturer will provide comprehensive documentation, including performance curves and installation guidelines, which can be invaluable during the selection process. Good customer support can assist you with troubleshooting and ensure that you get the most out of your investment in a quality submersible pump.
In summary, investing in quality submersible pumps is vital for the success of industrial applications. By focusing on construction materials, efficiency, maintenance, specific applications, and manufacturer support, you can make an informed decision that enhances your operational efficiency and reliability.
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha