-
Products
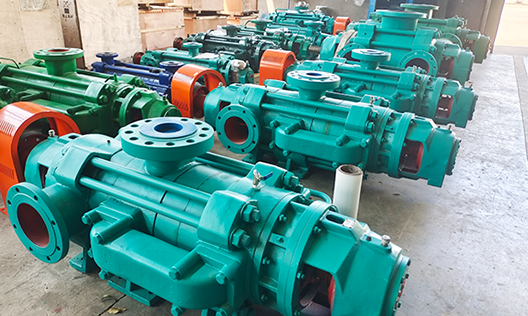
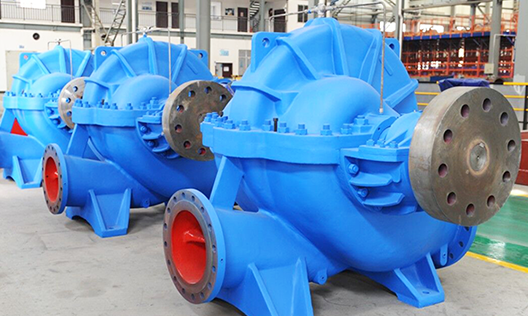
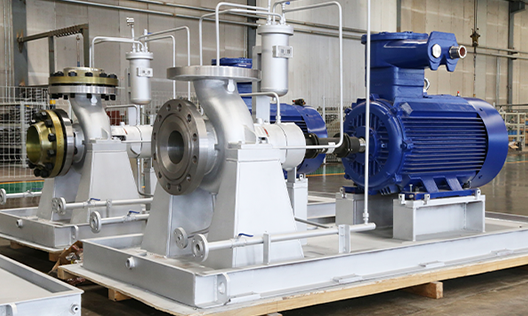
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
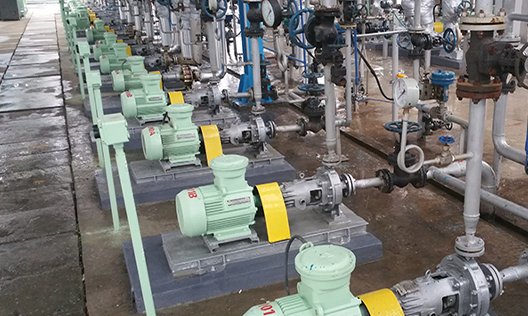
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Technical Specifications and Practical Selection Guide for Packing Seal Technology in Multi-stage Pumps Used in Mine Drainage
Publication Date:
2025-12-09
Author:
Source:


As the core equipment of mine drainage systems, the multi-stage pump for mining applications is a horizontal multi-section type. Centrifugal pump , also known as Multistage centrifugal pump Its core application scenario is the drainage of underground mine water (mine water containing fine particulate matter, but not slurry transport). According to coal industry standards. MT/T 114-2005 This pump is suitable for conveying fluids containing solid particles ≤ 1.5% , temperature ≤ 80 For mine water at ℃, the choice of sealing method directly determines the reliability of the equipment. The sand content in groundwater is typically... 500-5000mg/L Particle size 0.1-1.0mm ), under such operating conditions, mechanical seals (mechanical seals) are prone to failure due to particle jamming. Industry-verified failure rates exceed... 40% ; and the packing seal uses graphite packing rings. + The pressurized water circulation system can effectively adapt to particulate media and achieve... 8000 Stable operation for more than one hour. In this article, the manufacturer of multi-stage pumps for mining applications... Changsha Zhonglian Pump Industry Let’s share the technical specifications and practical selection guidelines for packing seal technology used in multi-stage pumps for mine drainage, for reference by user organizations.

I. Operating Condition Characteristics and Mandatory Requirements for Sealing Technology
1. Particle characteristics influence
Sediment content of groundwater >1000 mg/L At this time, particles easily become embedded in the mechanical seal surface, leading to seal failure and pump body leakage.
The packing seal uses flexible graphite packing rings, in combination with... 0.1-0.3MPa Pressure water circulation cools the system, forming a dynamic sealing layer that prevents particle intrusion.
2. Sealed structural design
The stuffing box shall be equipped with an independent water-seal system (not a self-circulating system within the pump body). Pressurized water is injected into the sealing chamber to continuously flush the particles.
Adjust the packing tightness to a “slightly permeable state.” 1-2 Drop / seconds), excessive tightness leads to accelerated wear, while excessive looseness results in leakage.
II. The selection must strictly match the actual operating conditions of the mine to avoid indiscriminate application.
III. Maintenance Essentials and Industry Practices
1. Gland Maintenance
Clean the packing fouling quarterly (flush the packing chamber with high-pressure water);
Check whether the pressurized water circulation pipeline is blocked (a blockage will lead to sealing failure).
2. Material matching
Sediment concentration >1500mg/L : The flow passage components adopt Cr27 High-chromium cast iron (enhanced wear resistance) 30% );
Acidic groundwater ( pH < 6 ): The pump body is made of duplex stainless steel (to prevent corrosion and perforation).
3. Pitfall Guide
The use of “submersible pumps” is prohibited in mine drainage applications (all multistage pumps are vertical). / Horizontal structure);
Reject “machine seal” + The “double-seal with filler” solution (particles can easily cause both seals to fail simultaneously).
IV. Technical Value and Economic Benefits
The scientifically selected packed seal multistage pump can achieve:
Reduced failure rate: from mechanical seals 30%+ Drop to 5% The following;
Operational and maintenance cost savings: Average annual reduction in downtime losses 25 Ten thousand yuan (according to 10 Tai Pump Calculation);
Security and Compliance Assurance: Meets the continuous operation requirements for drainage systems stipulated in the "Regulations on Safe Production in Coal Mines."
Case: A gold mine in Yunnan 2023 Replace the packing seal annually. MD After the series of pumps, the drainage system has been running continuously for over... 2000 Hours of operation without any downtime incidents caused by seal failure have been certified as a provincial-level safety benchmark case.
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha