-
Products
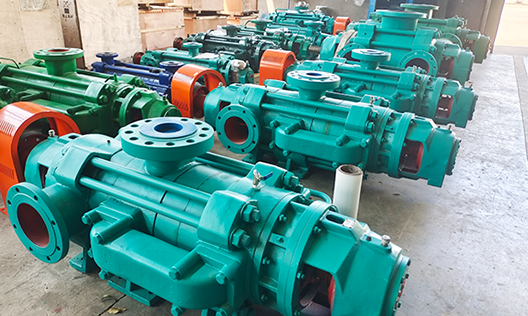
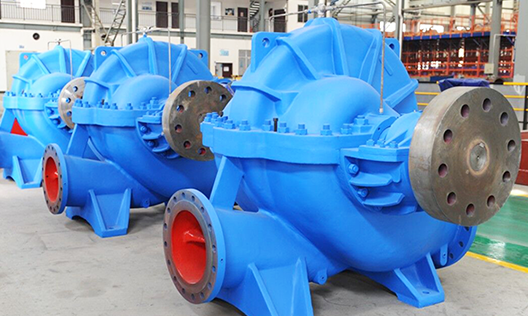
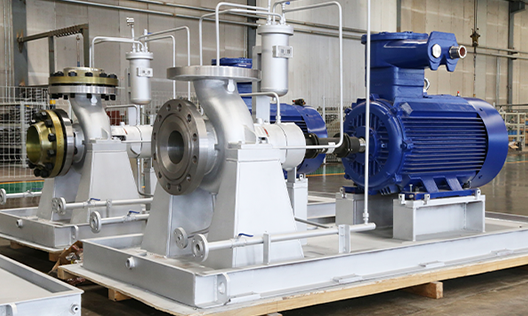
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
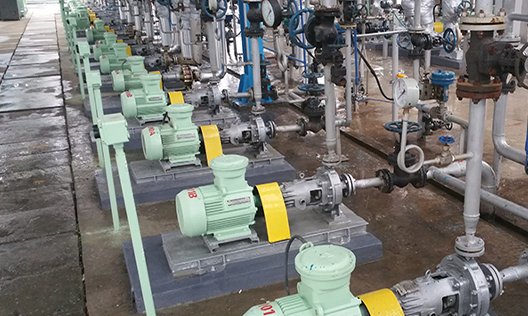
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Application and Technical Advantages of Multistage Centrifugal Pumps in Coal Mine Drainage
Publication Date:
2025-12-08
Author:
Source:


In coal mine production, Multistage centrifugal pump It is the core equipment for critical processes such as mine drainage and coal slurry transportation, and its stable operation directly affects mine safety, production continuity, and the protection of the working environment. With technological advancements, modern multistage pumps have been continuously optimized in terms of efficiency, reliability, and ease of maintenance and operation, making them indispensable fluid-handling equipment in the coal mining industry. In the industry, they are often referred to as... Mine multistage pump In this article, the manufacturer of multistage centrifugal pumps... Changsha Zhonglian Pump Industry Let me provide a detailed introduction to the application and technical advantages of multistage centrifugal pumps in coal mine drainage systems.

I. High hydraulic efficiency meets high-head requirements.
Multistage pumps for mining applications achieve high head output by connecting multiple impellers in series, effectively lifting liquids to the surface or to designated process locations while maintaining a reasonable flow rate. In mine water drainage, these pumps can rapidly remove groundwater, preventing water accumulation from compromising roadway stability. In coal washing and transportation processes, they can also be used to convey coal slurry with low solid content, thereby supporting the efficient operation of production workflows. Their hydraulic models are typically designed based on nationally recommended standards for high efficiency and energy conservation, resulting in superior operational efficiency compared to conventional single-stage pumps.
2. Reliable structure, suitable for harsh operating conditions.
Coal mine environments typically feature high humidity, dust, corrosive gases, and continuous operational requirements. To address these challenges, multistage pumps for mining applications are commonly manufactured using high-strength cast steel or stainless steel for both the pump body and rotor components, with wear-resistant treatments applied to the flow surfaces. Bearing systems often incorporate heavy-duty rolling bearings or sliding bearings, paired with either forced lubrication or grease lubrication methods, to ensure long-term stable operation. Some models—such as those compliant with... API610 Standard MDP Self-balancing horizontal multistage pump ) It adopts an axial-force-free design, reducing rotor wear, significantly extending trouble-free operating time, and lowering lifecycle maintenance costs.
III. Intelligent Control Enhances Operation and Maintenance Levels
Currently, mainstream multi-stage pumps for mining applications have integrated sensor interfaces for pressure, temperature, vibration, and other parameters, supporting compatibility with... PLC or DCS System integration enables remote start-up and shutdown, operational status monitoring, and early fault warnings. Automated control not only reduces the frequency of manual intervention but also lowers safety risks caused by operational errors or delayed responses, aligning with the trend toward intelligent mine development.
IV. Energy Conservation and Environmental Protection Support Sustainable Development
By optimizing the impeller profile, reducing internal leakage, and adopting high-efficiency motors, modern multistage pumps consume less energy under the same operating conditions. Meanwhile, improvements in sealing structures—such as replacing gland seals with mechanical seals—effectively reduce leakage, thereby minimizing water resource waste and environmental pollution.
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha