Customer Case
The choice of tens of thousands+customers.
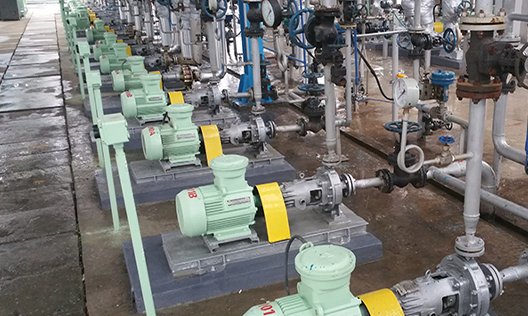
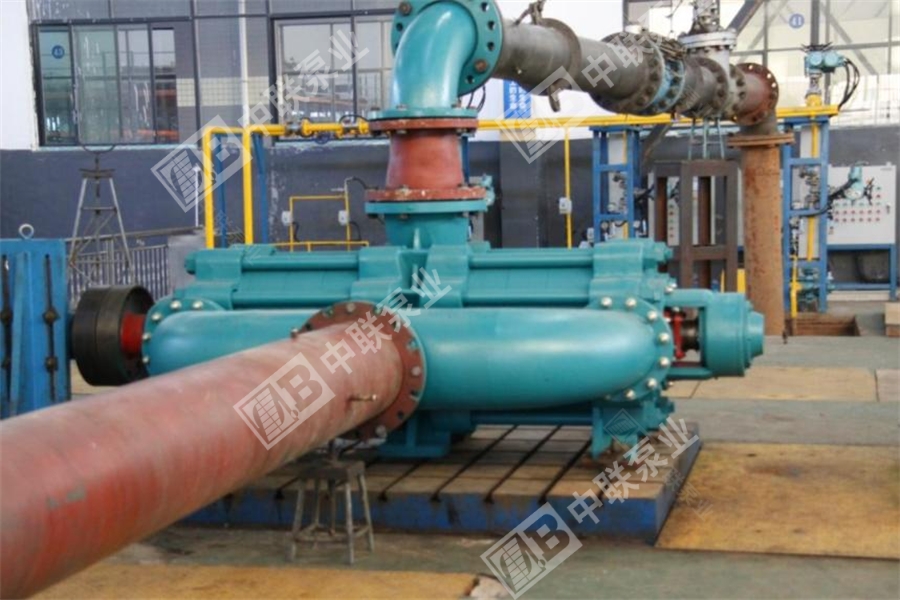
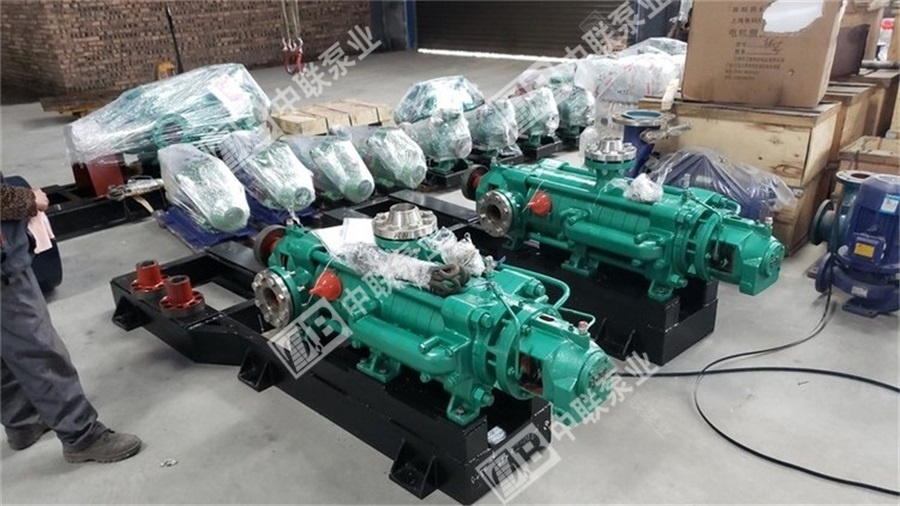
The sales department of Zhonglian Pump Industry received an inquiry from a project in Huili County, Sichuan Province, seeking pump equipment supplies for a domestic water supply project. After more than three months of on-site inspections, Zhonglian Pump Industry successfully won the bid for this project, thanks to its exceptional product quality, expertly tailored solutions, and outstanding cost-effectiveness. The winning bid includes two sets of D85-80x12(P) self-balancing multistage clear water pumps, along with the provision of dedicated motors and other related equipment.
The waste heat recovery project for Henan-based Coal & Coke Co., Ltd., a long-standing client, is a key component of their green production initiative and equipment procurement project. Leveraging years of accumulated expertise in boiler feedwater pump technology, along with its strong customization capabilities and extensive engineering application experience, Zhonglian Pump Industry has successfully secured the contract to supply the DG12-80×10P (self-balancing multistage boiler feedwater pump) for this project.
To meet the demands for high head and corrosion-resistant equipment, an oilfield exploration company selected a DF46-80*11(P) stainless steel self-balancing multistage centrifugal pump—produced by Zhonglian Pump Industry—with a flow rate of 45 m³/h and a head of 880 m—as the lean amine solution circulation pump.
Recently, Zhonglian Pump Industry reached a cooperation agreement with a power plant in Xinjiang to supply it with DG85-80*9P self-balancing boiler feedwater pumps for its boiler feedwater system. The equipment has now completed production, transportation, and on-site installation and commissioning, and has officially been put into stable operation. The boiler upgrade project at this power plant requires the pumps to be suitable for high-temperature and high-pressure operating conditions. The core requirement is continuous and stable delivery of deaerated water, with a medium temperature not exceeding 105℃, an inlet pressure no greater than 0.6 MPa, and the ability to meet the specified performance parameters of a rated head of 720 meters and a flow rate of 85 m³/h. Given that the lowest winter temperature in Xinjiang can drop as low as -20℃, the equipment must also demonstrate reliable starting performance under low-temperature conditions and comply with the GB/T12145-2016 standards for steam quality in thermal power generating units.
To ensure the safety of drainage operations and the continuity of production in deep‑mining operations, this manganese mine has launched a technical upgrade project for its underground central pump room. After conducting open bidding, technical evaluations, and on-site factory inspections, the mine ultimately partnered with Changsha Zoomlion Pump Industry Co., Ltd., a manufacturer of multistage pumps that holds mining safety certification. The company signed a contract to procure MD155-67x7P explosion‑proof, self‑balancing, horizontal multistage centrifugal pumps for use as the core equipment in its deep‑drainage system.
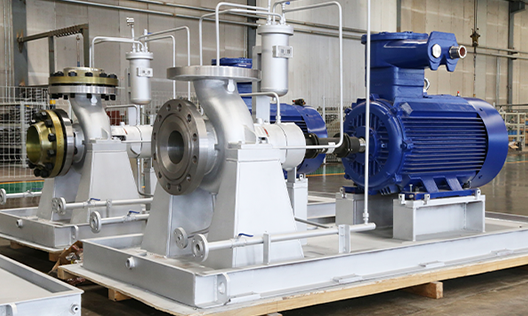
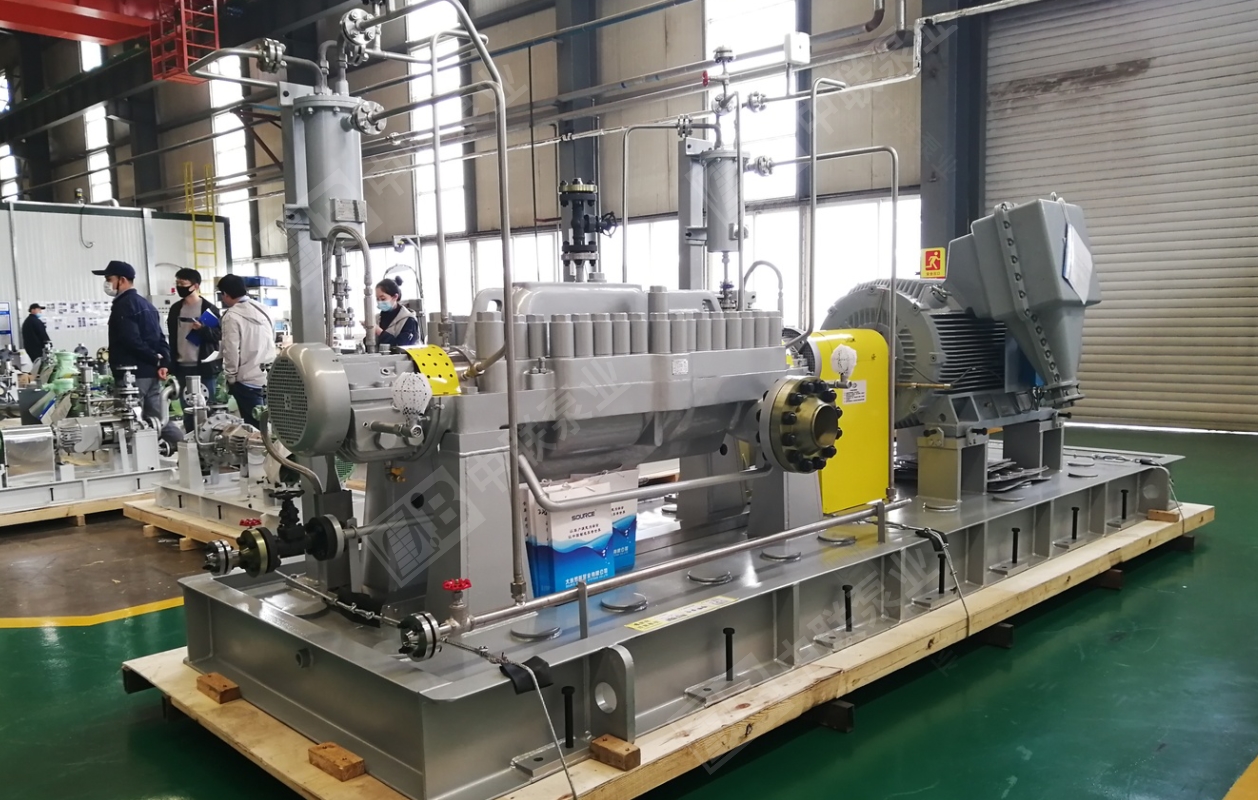
API 610 BB3 Configuration KHP-Type Multistage Split-Case Pump
The KHP pump is a horizontal, mid-split, multistage pump developed by Changsha Zoomlion Pump Industry in accordance with the API 610 standard. Built upon an optimally selected hydraulic model and leveraging CFD fluid dynamics simulations and computer-aided design techniques, it represents a new generation of high-pressure multistage pumps that offer high efficiency, energy savings, robust durability, and ease of maintenance.
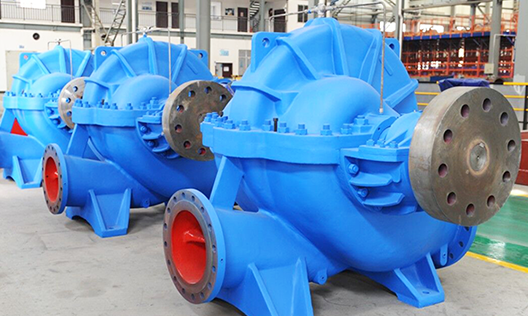
D/F/Y/MSK Series Horizontal Split-Case Multistage Pumps
The DSK, DFSK, DYSK, and MDSK series of horizontal, mid-open multistage pumps represent a new generation of large-scale, horizontally configured, mid-open multistage centrifugal pumps independently developed by Changsha Zhonglian Pump Industry. This product line features a dual-inlet design with symmetrically arranged impeller and rotor components; after the fluid flows through the final-stage volute casing and pressure chamber on both sides, it exits, forming a parallel-flow configuration. The pump boasts numerous outstanding characteristics, including high flow rate, high head, compact and aesthetically pleasing design, high efficiency and energy savings, a broad high-efficiency operating range, excellent cavitation resistance, smooth operation, convenient maintenance, and reliable performance. As a national high-tech product, it fills a critical gap in China’s market for high-parameter multistage centrifugal pumps with large flow rates and high heads. These pumps are widely used in industrial cooling-water circulation, secondary pressurization pumping stations for high-altitude water intake, agricultural irrigation, river-water intake, flood drainage, municipal engineering, and other applications.