-
Products
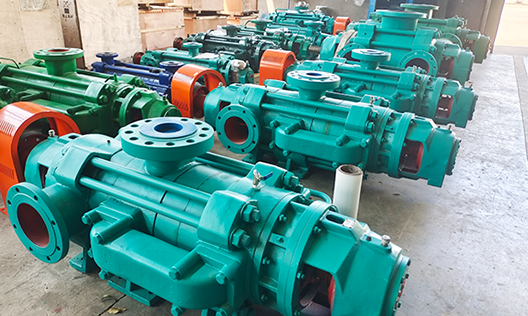
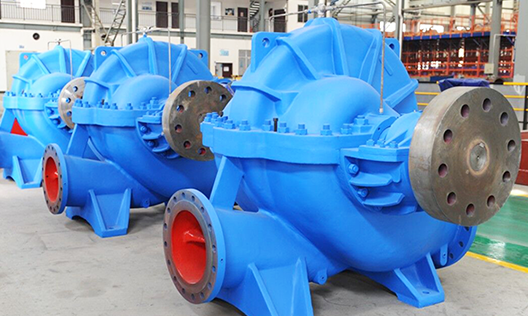
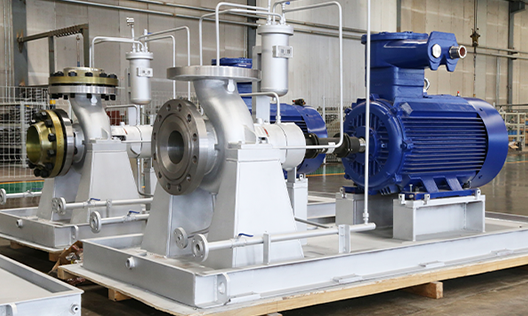
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
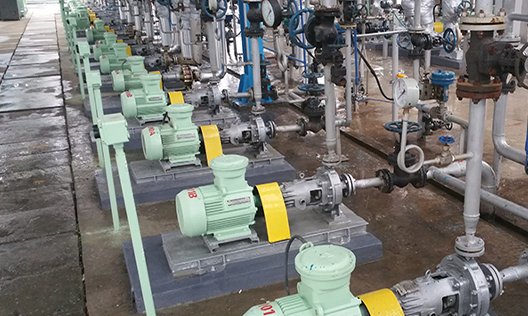
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Understanding Multistage Pumps: Your Essential Guide
Publication Date:
2026-09-23
Author:
Source:


One of the primary advantages of multistage pumps is their efficiency. By utilizing multiple stages, these pumps can achieve a higher total head than their single-stage counterparts, making them ideal for applications that require the elevation of fluids across significant vertical distances. This characteristic is particularly beneficial in industries such as water treatment, chemical processing, and mining, where fluid transport can be both challenging and energy-intensive.
In addition to their efficiency, multistage pumps offer versatility in fluid handling. They can be designed to accommodate various types of fluids, including clean water, chemicals, and other industrial liquids. Furthermore, the ability to adjust the number of stages allows for customization based on specific operational requirements, ensuring optimal performance for different applications.
When it comes to operation, multistage pumps rely on a series of impellers and diffusers, each contributing to the overall pressure increase. As the fluid enters the first impeller, kinetic energy is imparted to the fluid, which is then converted into pressure as it flows through the diffuser. The fluid continues this process through subsequent stages, with each stage providing additional energy and pressure until the desired output is achieved.
Maintenance of multistage pumps is crucial for their longevity and reliability. Regular inspections and servicing can help detect issues such as wear and tear on the impellers or seals, which can lead to decreased efficiency or operational failures. It is also essential to ensure that the pump is adequately sized for its application to avoid excessive wear and potential damage.
In conclusion, multistage pumps are vital tools in various industries, offering high efficiency, versatility, and reliable performance. Understanding their operational principles and benefits can help professionals make informed decisions when selecting the appropriate pumping solutions for their specific needs.
Previous:
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha