-
Products
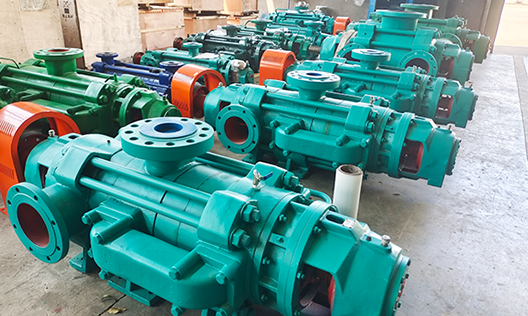
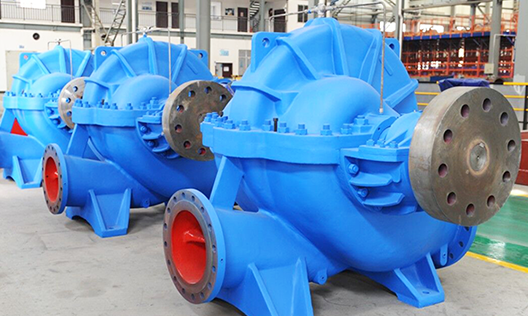
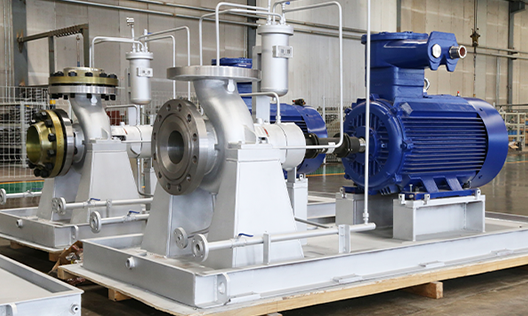
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
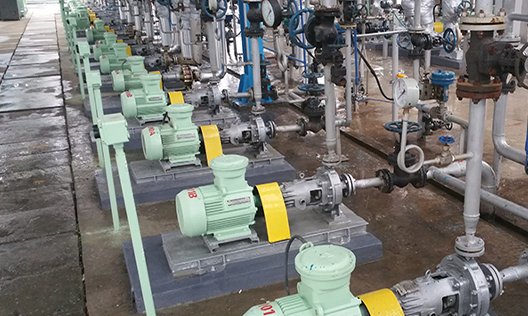
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Mining drainage pump
Publication Date:
2025-09-05
Author:
Source:


Mining drainage pumps are primarily used for draining water from the central pump rooms in coal mines, as well as for emergency flood control and post-flood recovery drainage after water inundation disasters. Multi-stage centrifugal pumps are commonly employed for these purposes. MD Series Mining Drainage Pumps This is our factory's newly developed product, which not only boasts high efficiency and excellent cavitation performance, but also ensures smooth, reliable operation. It widely utilizes alloy wear-resistant cast iron materials, making it ideal for transporting neutral mine water—up to 80°C—in coal mines, as well as other similar wastewater applications. Primarily suited for coal mine wastewater and comparable scenarios like tunnel drainage and urban sewage systems, this series of mining drainage pumps has already passed the necessary certifications. National Coal and Mine Safety Certification , featuring the dedicated "MA" and "KA" certifications for mining applications.
↑Click the image to learn more Product details of the MD-type mining pump (mining multistage centrifugal pump) and Price Information ↑
Mining drainage pump models
I. MD-Type Horizontal Mine-Use Multistage Centrifugal Drainage Pump
MD-Type Horizontal Mine-Use Multistage Centrifugal Drainage Pump This is a horizontal, single-suction, sectional multistage centrifugal pump designed for conveying neutral mine water containing solid particles no more than 1.5% by volume (with particle size smaller than 0.5 mm), as well as other similar wastewater. It incorporates a hydraulic model that aligns with the nation’s recommended efficient and energy-saving products, placing it at the forefront of technology within the industry. The pump boasts advantages such as high efficiency, a wide performance range, safe and stable operation, low noise levels, extended service life, and convenient installation and maintenance.
The MD horizontal mining multistage centrifugal drainage pump features a hydraulic balancing device—a balance disc—that fully and automatically counterbalances axial forces. This device consists of four key components: the balance plate, balance disc, balance sleeve, and balance retaining sleeve. The main components include the suction section, middle section, discharge section, impeller, guide vanes, discharge-section guide vanes, shaft, sealing rings, balance rings, shaft sleeves, tail cover, and bearing housing. Notably, the suction section, middle section, guide vane plates, discharge-section guide vanes, discharge section, and tail cover are all made of cast iron, collectively forming the pump’s working chamber. All flow-through components are manufactured using precision casting, ensuring precise flow channel dimensions and exceptional surface smoothness, which in turn delivers excellent energy-saving performance.
II. MDP-Type Self-Balancing Mine-Use Multistage Drainage Pump
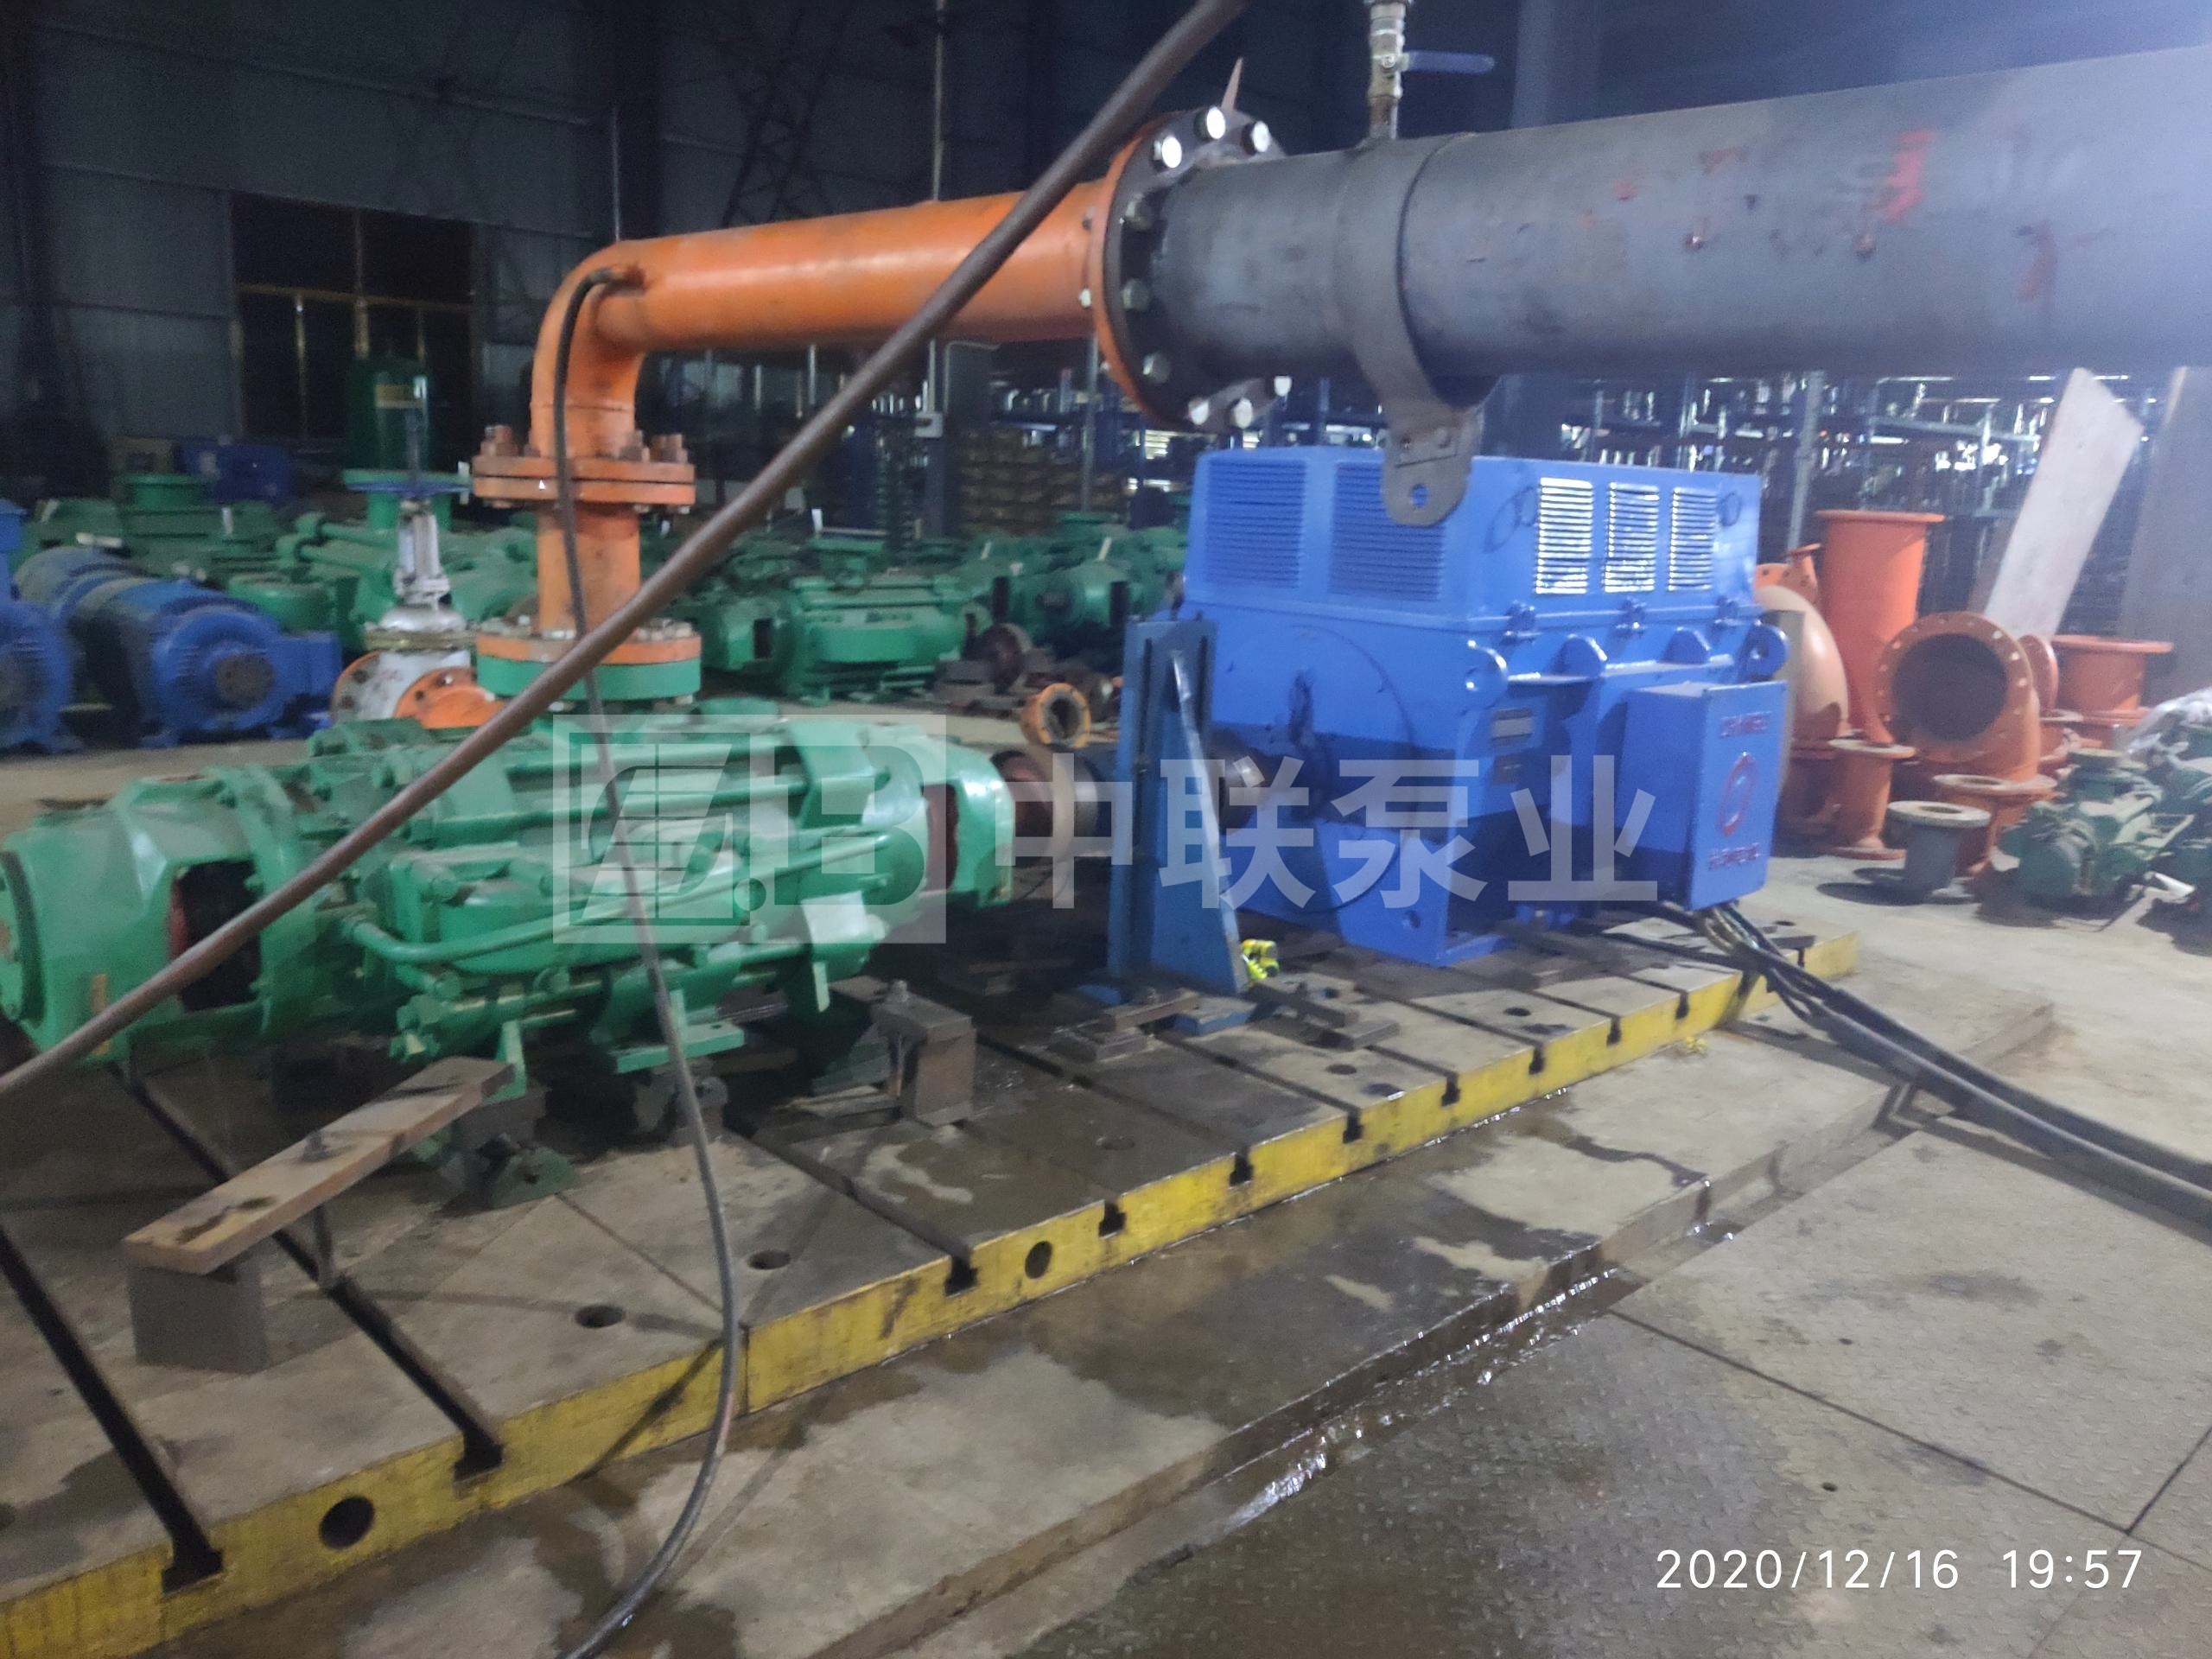
MDP-Type Self-Balancing Mine-Use Multistage Drainage Pump This is the latest self-balancing, high-head mining multistage centrifugal pump developed by Zhonglian Pump Industry, designed for conveying medium-sized mine water intake and other similar wastewater containing particle content of up to 1.5%, with particle size no larger than 1.3 mm, and operating at temperatures ranging from -20°C to 80°C. In addition to its exceptional wear resistance, this pump boasts high efficiency, excellent cavitation performance, stable and reliable operation, extended service life, and the ability to deliver high head at low rotational speeds. Featuring a unique self-balancing design—specifically, a horizontal, multi-stage, highly efficient, and energy-saving centrifugal pump configuration—the pump incorporates symmetrically arranged impellers, eliminating the need for a traditional balance disc system. As a result, the pump rotor operates without axial movement, ensuring that the flow passages remain perfectly aligned at all times, thereby maintaining optimal efficiency throughout operation. This design also contributes to a flat efficiency curve, enabling the pump to run continuously for up to 8,000 hours without any failures. Furthermore, the pump employs an advanced modular design, making its impellers, rotating components, and other interchangeable parts highly compatible and easily replaceable, enhancing both maintenance flexibility and operational convenience.

The following image shows a large mining company in Hebei Province using our company’s MDP-type self-balancing, mine-specific multistage centrifugal drainage pump. Since its purchase and installation in 2015, the pump has been running smoothly and reliably until today. We have numerous similar success stories with other customers. Our company has established collaborative partnerships with several universities and research institutions, enabling us to continuously innovate and manufacture self-balancing multistage pumps. To date, we’ve secured multiple patents and accumulated extensive industry experience, earning widespread acclaim from clients. Over the years, through continuous production cycles and valuable market feedback, our products have undergone constant refinement and upgrades. Today, they have reached a highly advanced stage in terms of manufacturing precision, energy efficiency, operational reliability, and overall quality—making them not only exceptionally competitive but also offering outstanding value for money in the market. Mining multi-stage centrifugal drainage pump.


Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha