-
Products
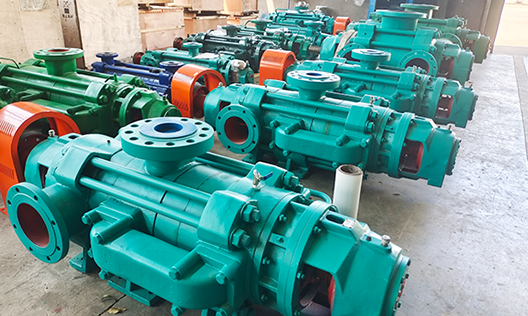
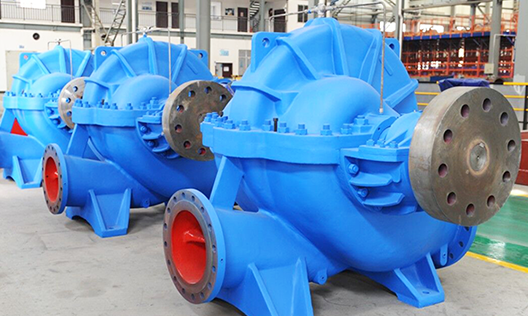
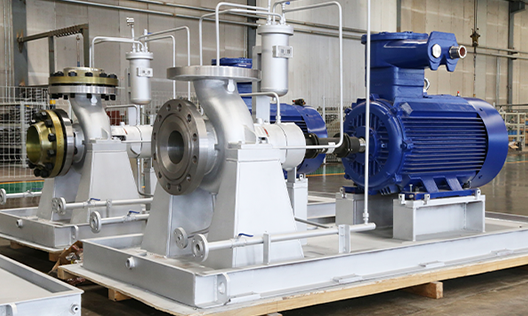
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
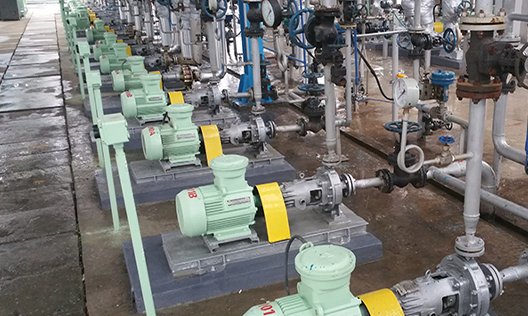
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
High-pressure multistage pump
Publication Date:
2025-09-05
Author:
Source:


A high-pressure multistage pump, officially known as a high-pressure multistage centrifugal pump, is a type of centrifugal pump capable of delivering water to exceptionally high head ranges. The key distinction between this pump and a single-stage centrifugal pump lies in the number of impellers—precisely, it's the number of impellers that determines the pump's pressure and head capacity. Additionally, structurally, high-pressure multistage centrifugal pumps are more complex than their single-stage counterparts, demanding higher standards in design and manufacturing processes. As a result, producing high-quality multistage pumps with superior performance represents a significant technical challenge for manufacturers. Hunan Province, renowned for its well-developed pump industry chain, boasts numerous pump manufacturers. Each company often focuses on different types of pumps based on their strengths and market positioning. Among them, Changsha Zoomlion Pump Industry Co., Ltd. stands out as a specialist dedicated to the research, development, production, and sales of high-pressure multistage pumps. With 13 independently owned intellectual property rights under its belt, the company has established itself as a leading manufacturer of high-pressure multistage pumps in Central China.

Our company’s high-pressure multistage pumps are primarily categorized into mining multistage pumps, multistage boiler feedwater pumps, multistage chemical pumps, and multistage oil pumps, depending on their application type. Given that these high-pressure multistage pumps offer an exceptionally wide range—both in terms of flow rate and head capacity—their applications effectively cover water treatment requirements across virtually every industry. Now, let’s explore these various types of high-pressure multistage pumps together with the editor from Zhonglian Pump Industry!
Mining multistage pump
I. Overview of High-Pressure Mining Multistage Pumps
High pressure Mining multistage pump It is a horizontal, single-suction, multistage sectional/segmented centrifugal pump. Among multistage pump manufacturers, Zhonglian Pump Industry has adopted the hydraulic model of an efficient and energy-saving product recommended by the national standards, developing a specialized high-efficiency, high-pressure multistage centrifugal pump tailored specifically for the mining industry—technology that places our company at the forefront of the sector. Our company produces two main types of mining multistage pumps: MD-Type Wear-Resistant Mining Multistage Pump And MDP-Type Self-Balancing Mine-Use Multistage Pump Both models of the high-pressure mining multistage pumps have fully passed both Coal Safety Certification and Mine Safety Certification.

MD-Type Wear-Resistant Mining Multistage Pump
II. Applications for High-Pressure Mining Multistage Pumps
High-pressure mining multistage pumps are designed for conveying neutral mine water containing solid particles at a concentration of no more than 1.5% (with particle size smaller than 0.5 mm) and other similar wastewater. The temperature of the medium being pumped must not exceed 80°C, making these pumps suitable for applications such as steel plants, mine drainage, and sewage transport.
1. Under clear water conditions (with solid particle content below 0.1%), the equipment can operate for 5,000 hours without major maintenance, with efficiency degradation not exceeding 6%.
2. Under sewage conditions containing solid particles at levels below 0.1% to 1%, the system can operate for 3,000 hours without major maintenance, with efficiency degradation not exceeding 5%.
3. Under wastewater conditions containing 1–1.5% solid particles, the system can operate for 2000 hours without major maintenance, with efficiency degradation not exceeding 6%.

MDP-Type Self-Balancing Mine-Use Multistage Pump
III. Advantages of High-Pressure Mining Multistage Pump Products
Our company produces high-head, multi-stage mining pumps—high-capacity water pumps capable of reaching an impressive head of up to 1,800 meters. These pumps boast exceptional efficiency, a wide performance range, smooth and reliable operation, low noise levels, extended service life, and convenient installation and maintenance. They are perfectly tailored to meet the diverse needs of various mining enterprises. Additionally, we can customize explosion-proof, integrated motor-driven multi-stage mining pumps specifically designed for your mine type and tailored to address any hazardous gases or materials present on-site. This ensures the safety of both personnel and assets at your facility.
High-pressure multi-stage boiler feedwater pump
I. Overview of High-Pressure Multi-Stage Boiler Feed Pumps
High-pressure multi-stage boiler feedwater pump For horizontal multistage single-suction sectional-type Centrifugal pump , it is one of the most critical boiler pumps used in power plants and heating systems. The task of the multistage boiler feedwater pump is to take deaerated feedwater—water that has been heated to a certain temperature and freed from dissolved oxygen—from the deaerator storage tank, increase its pressure, and then deliver it to the boiler, ensuring that the water level inside the boiler is maintained at the required technical height. Our company’s high-pressure multistage boiler feedwater pumps are divided into DG-Type Boiler Feedwater Pump And DGP-Type Self-Balanced Boiler Feedwater Pump 。

II. Applications of High-Pressure Multi-Stage Boiler Feed Pumps
Primarily used for conveying clear water or liquids with physicochemical properties similar to water, at temperatures ranging from -20°C to 210°C—and free of solid particles. Suitable for medium-, low-, and high-pressure water supply applications.
III. Advantages of High-Pressure Multi-Stage Boiler Feed Pump Products
The high-pressure multi-stage boiler feedwater pump has replaced the older model. GC-Type Boiler Feedwater Pump , this is a highly efficient and energy-saving product specifically designed as a complementary solution for the upgraded and renovated series of industrial steam boilers. It is suitable not only for feedwater applications in medium- and low-pressure boilers but also ideal for high-lift water transportation systems in factories and urban areas. Structurally, it features a horizontal installation and multi-stage design, ensuring smooth operation while offering convenient installation and maintenance—making it a widely adopted choice in today’s market. Boiler water pump 。

DGP-Type Self-Balanced Boiler Feedwater Pump
High-pressure multi-stage chemical pump
I. Overview of High-Pressure Multistage Chemical Pumps
High-pressure multi-stage chemical pump Single-suction, multistage, segmental Multistage centrifugal pump , is my company in Type D Clear Water Multistage Pump Based on this foundation, an improved design of a horizontal centrifugal multistage Stainless Steel Chemical Pump This pump adopts the nationally recommended hydraulic model, featuring high efficiency, a broad performance range, stable and smooth operation, low noise levels, extended service life, and convenient installation and maintenance. Primarily designed for conveying corrosive media such as strong acids and strong bases, it is one of the most commonly used corrosion-resistant chemical pumps in industries like metallurgy and chemical engineering. Additionally, it can be perfectly paired with explosion-proof motors for draining corrosive wastewater from coal mines or mining sites. Our company’s high-pressure multistage chemical pumps are categorized into DF-Type Corrosion-Resistant Multistage Chemical Pump And DFP-Type Self-Balanced Multistage Chemical Pump 。

DF-Type Corrosion-Resistant Multistage Chemical Pump
II. Applications of High-Pressure Multistage Chemical Pumps
Suitable for conveying clear water or media with stable physicochemical properties, where solid particles do not exceed 0.1% by volume and have a particle size of ≤2mm—similar to clear water—at temperatures ranging from -20℃ to 105℃. It can also be used to transport corrosive liquids with a pH range of 5 to 10, as well as other chemical solutions.

DFP-Type Self-Balanced Multistage Chemical Pump
III. Advantages of High-Pressure Multi-Stage Chemical Pump Products
1. High Efficiency and Energy Savings: We adhere to specialized manufacturing practices, employing unique approaches in product model selection, mold fabrication, and the casting process for hydraulic components. All flow-through parts are produced using advanced precision casting techniques, ensuring precise flow channel dimensions and exceptional surface smoothness. As a result, our pumps demonstrate an average efficiency that is more than 2% higher than that of conventional multi-stage pumps currently available on the market, delivering outstanding energy-saving performance.
2. Advanced Process Equipment: To ensure the assembly performance of our products, our company has imported state-of-the-art component cleaning equipment from overseas. Each part undergoes certified cleaning before final assembly. In addition to standard practices such as material inspection, hydrostatic pressure testing, and static balance checks, all pump rotor components rated at Level 6 or higher are subjected to a secondary inspection following partial assembly, focusing on shaft runout—specifically, ensuring that the runout value remains within 5 microns. These components then proceed to dynamic balancing tests conducted according to G2.5 standards. Finally, after complete assembly, we perform another round of inspections to verify both shaft runout and axial movement relative to the coupling, thereby guaranteeing the highest quality in product assembly.
3. Unique Structure: An O-ring seal is installed at the mating surface between the balance ring and the pump, preventing high-pressure water from entering the balance chamber and compromising the balancing effect of the balance disc. This design reduces wear on the balance disc, thereby extending the product's service life.
4. Reasonably select materials: Depending on different user requirements, the balance disc and balance ring can be made from hard alloy overlay welding, alloy steel, or QT600Mn2 ductile cast iron alloy—materials that offer high surface hardness and excellent wear resistance, thereby extending the product's service life.
5. Excellent Surface Quality: Utilizing precision casting mold technology and automated spray painting machines for paint application, these products boast superior surface quality and an aesthetically pleasing appearance.
High-pressure multi-stage oil pump
I. Overview of High-Pressure Multi-Stage Oil Pumps
High-pressure multi-stage oil pump This is a high-temperature, high-pressure product designed and manufactured by our company, specifically for the petrochemical industry. Multi-stage pump , it adopts the highly efficient and energy-saving hydraulic model recommended by the nation, significantly enhancing reliability while dramatically reducing user maintenance costs, thereby lowering the pump's life-cycle costs. Our company’s high-pressure multistage chemical pumps are divided into DY-Type High-Pressure Multistage Centrifugal Oil Pump And DYP-Type Self-Balanced Multistage Oil Pump 。

DY-Type High-Pressure Multistage Centrifugal Oil Pump
II. Applications of High-Pressure Multi-stage Oil Pumps
Used to convey petroleum and petroleum products with a viscosity of less than 120 centistokes, free of solid particles. The medium temperature ranges from –20°C to 150°C, and the allowable inlet pressure is up to 0.6 MPa.
III. Advantages of High-Pressure Multi-Stage Oil Pumps
The quality of assembly for the DY-type high-pressure multistage oil pump significantly impacts its performance—particularly the relative positioning between the outlet of each impeller and the inlet of the guide vanes. When assembled properly, this pump offers numerous advantages, including high efficiency and energy savings, a wide performance range, safe and stable operation, low noise levels, extended service life, and convenient installation and maintenance.
The DYP-type self-balancing multistage oil pump features a safe sealing design. Depending on the pressure and structural requirements, the pump casing employs either a metal-to-metal hard seal or an O-ring seal. This design offers advantages such as uniform flow, simple construction, wide-ranging flow and head capabilities, and convenient maintenance. As a result, the pump is widely used in petrochemicals, oilfield surface engineering, and crude oil injection systems. The DYP-type self-balancing multistage pump innovatively redefines the traditional multistage centrifugal pump structure by eliminating Conventional Multistage Pump The axial force balancing device, which utilizes a symmetrically arranged Impeller The rotor components' opposing forces counterbalance the axial force, effectively eliminating axial movement. This prevents efficiency losses caused by disc friction and backflow in the balance disc during operation. As a result, the pump achieves an efficiency 3–12% higher than that of conventional multi-stage pumps in the same category. Additionally, it completely addresses various failures—such as wear on the balance disc and its seat, or even rotor seizure—that typically arise from balance device malfunction—greatly extending the pump's service life.

Changsha Zoomlion Pump Industry promises our valued customers: If you encounter any issues with your pumps, feel free to call our 24-hour service hotline at 0731-88192288 anytime. Our dedicated service team will promptly log the issue into our customer management system, ensuring that all customer feedback and information are systematically organized and stored for efficient, fast, and seamless handling—and to save you valuable time!
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha