-
Products
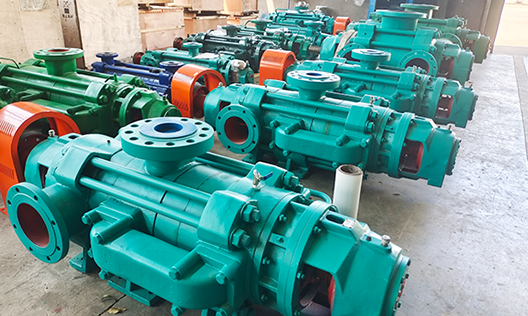
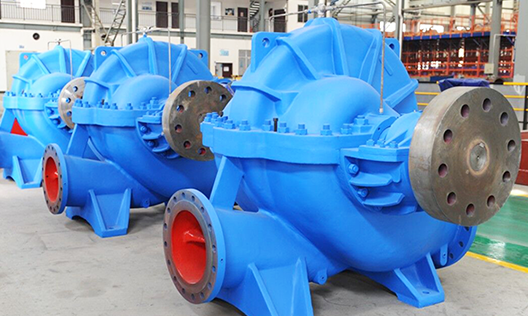
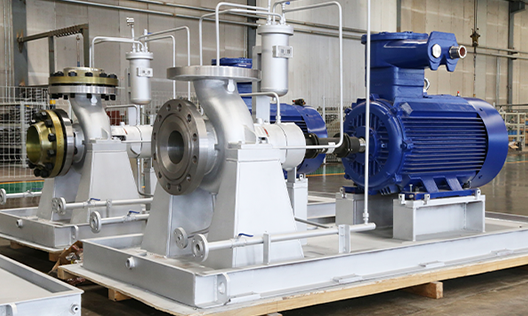
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
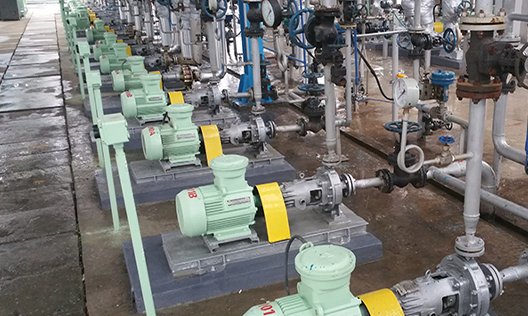
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Why does the usage rate of self-balancing multistage pumps account for such a large proportion in coal mines?
Publication Date:
2025-06-19
Author:
Source:


Self-balancing Multistage Pump Why does the usage rate in coal mines account for such a large proportion? It needs to be analyzed from several aspects. The structure of the self-balancing multistage pump itself is the most important reason, and it must also be combined with the characteristics of application conditions such as coal mines.
The environment in coal mines is usually harsh, possibly with high humidity, a lot of dust, and corrosive substances. Coal mines require a large amount of drainage and high-pressure liquid transportation, such as drainage systems underground or working fluids for hydraulic supports.
What advantages might the structure of the self-balancing multistage pump have? Multistage pumps usually provide higher lift, suitable for long-distance or high-pressure transportation. The self-balancing design may solve the axial force problem of traditional multistage pumps, reducing wear and maintenance costs. This is very important for coal mines because high equipment reliability can reduce downtime and improve production efficiency.

[For more information about models, parameters, selection, and quotation plans of self-balancing multistage pumps, you can click the image above to learn more]
In terms of safety, coal mines have high requirements for explosion-proof and reliability. The self-balancing multistage pump may be designed to meet these standards. Energy saving is also a factor; coal mines consume a lot of electricity, and efficient pumps can reduce operating costs. Additionally, policy support may promote the application of high-efficiency and energy-saving equipment.
Self-balancing Multistage Pump Features of axial force self-balancing, as well as discharge volume, pressure requirements, and environmental adaptability.
Considering all the above points, the usage rate of self-balancing multistage pumps in coal mines is higher!
Latest News
Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha