-
Products
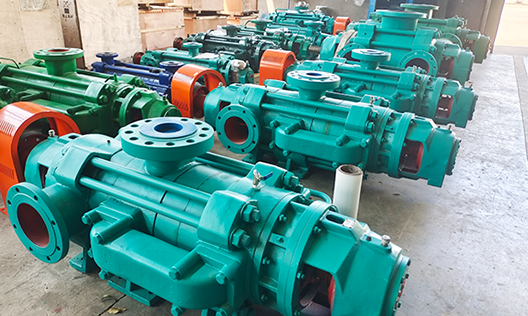
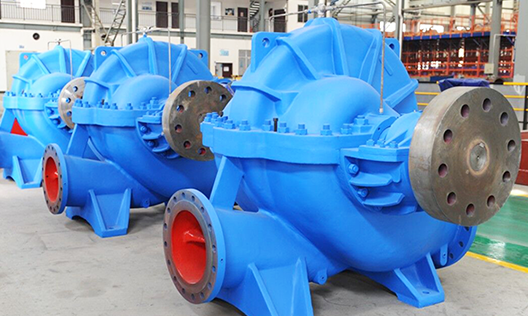
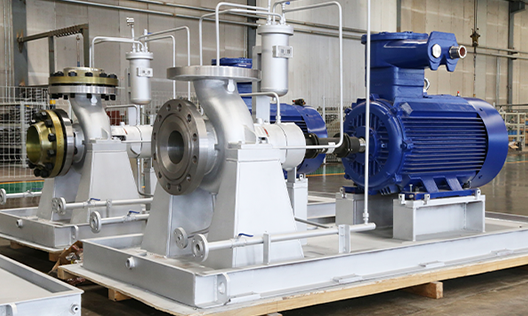
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
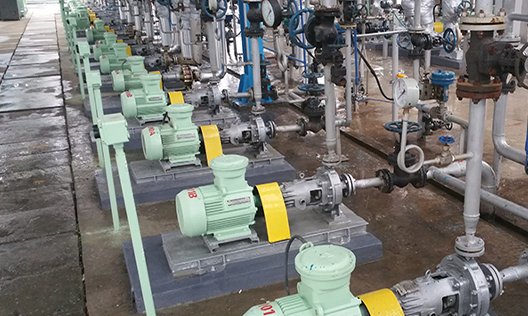
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Why are slurry pumps used in the coal mining industry? What role do slurry pumps play in the coal mining industry?
Publication Date:
2025-06-19
Author:
Source:


In the process of coal mining and production, Slurry pump As a key piece of equipment, it is involved in almost every stage from mine extraction to coal slime treatment. This special pump, capable of efficiently transporting high-concentration, highly abrasive solid-liquid mixed media, has become an indispensable "transport artery" in the coal mining industry due to its unique performance advantages.
So why is the slurry pump used in the coal mining industry? The media generated during coal production has the following characteristics, which make ordinary water pumps inadequate:
High solid content: The mixture of coal gangue, coal slime, and other materials produced during coal mining contains 30% to 70% solid particles, causing ordinary centrifugal pumps to clog or wear easily;
Strong abrasiveness: Coal slag particles are hard, and long-term erosion damages pump components;
Complex working conditions: The underground environment is humid and space is limited, and the media may contain acidic or alkaline components;
Environmental and safety requirements: Efficient treatment of coal slime water is needed to avoid pollution and the risk of mine flooding.
These characteristics require the conveying equipment to be wear-resistant, clog-resistant, corrosion-resistant, and highly reliable, and the targeted design of slurry pumps precisely meets these needs. And Slurry pump The following features can solve these pain points:
1. Efficient transportation of high-concentration solid-liquid mixtures
Structural optimization: Using wide-channel impellers and large-diameter designs to reduce the risk of clogging by large particles such as coal gangue and coal slime.
Power matching: High lift and large flow characteristics can meet the underground long-distance and high-drop transportation needs, such as transporting coal slime from the mining face to the surface treatment station.
2. Super wear resistance and corrosion resistance

[For more information on slurry pump models, parameters, selection, and quotation plans, please click the image above]
Material upgrade: Flow-through parts (such as impellers and liners) use high-chromium alloy, rubber lining, or ceramic coating, with a service life 3 to 5 times that of ordinary pumps.
Corrosion protection: For corrosive media such as sulfur-containing coal slime water, special coatings or duplex stainless steel materials are used to extend equipment life.
3. Ensuring production safety and environmental compliance
Rapid drainage: In case of mine water inrush or seepage, slurry pumps can quickly discharge accumulated water to prevent flooding accidents.
Closed-loop treatment of coal slime water: Cooperates with dehydration equipment to achieve coal slime recycling, wastewater purification, and compliant discharge, reducing environmental pollution.
For example: In the fully mechanized mining face, slurry pumps transport slurry containing coal gangue and broken coal to the surface washing plant, avoiding underground accumulation that affects operational safety.
Used in the medium circulation of coal washing plants for circulating magnetite powder and coal slime mixed media in heavy medium coal preparation systems, ensuring stable separation density.
Equipped with explosion-proof motors for mine drainage and emergency rescue, slurry pumps can operate safely in gas environments, used for daily drainage or emergency rescue during sudden water inrush events.
In tailings pond backfilling, washed tailings slurry is pumped to the tailings pond for centralized solid waste treatment, reducing the risk of surface subsidence.
Slurry pump The widespread application in the coal mining industry is essentially a targeted solution to the challenges of complex working conditions and harsh media. It not only ensures the efficiency and continuity of coal production but also plays a key role in safe production, resource recovery, and environmental protection. In the future, with the further integration of new materials and IoT technology, slurry pumps will continue to release value in the intelligent and green transformation of coal mines, becoming one of the core supporting devices for high-quality development in the industry.
Latest News
Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha