-
Products
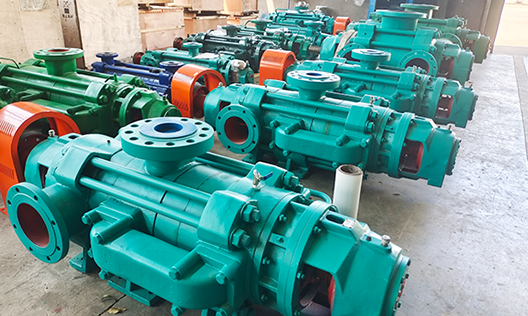
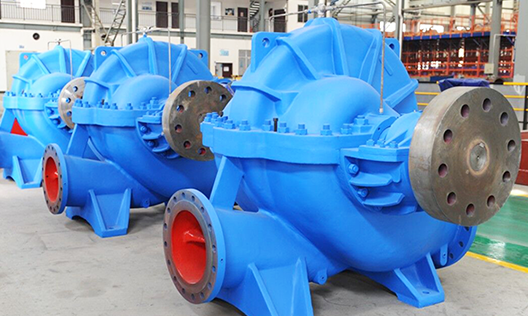
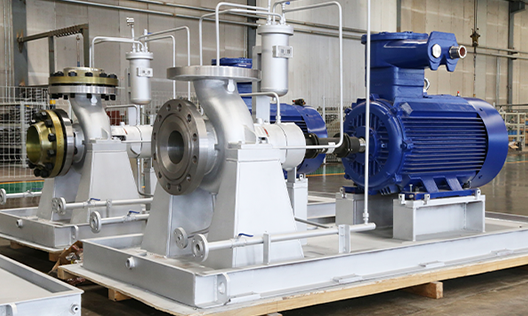
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
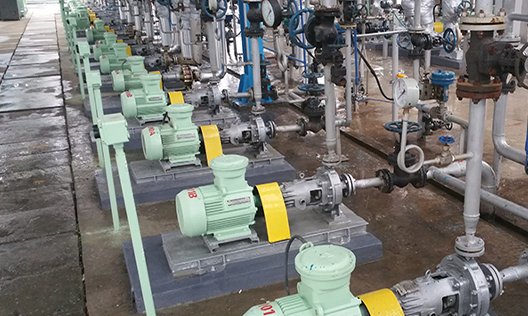
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Why does everyone choose self-balancing multi-stage pumps for mining?
Publication Date:
2025-06-19
Author:
Source:


Why does everyone choose Self-balancing mining multistage pumps ? When users purchase industrial water pumps, they compare multiple options, but industry comparisons show that over 70% of users buying mining multistage pumps choose self-balancing mining multistage pumps. Why is that? Today, the editor will explain the reasons in detail from the following aspects.
Self-balancing mining multistage pumps have become the preferred equipment in mining, coal mines, and other fields due to their revolutionary technological breakthroughs and excellent performance. We
can analyze their core advantages from multiple dimensions such as technology, economy, safety, and operation & maintenance to explain why choose self-balancing mining multistage pumps.
1. From the structural perspective: eliminating the fatal flaws of traditional pumps
1. Axial force self-balancing technology
Through symmetrical impeller arrangement (forward/reverse impeller groups), the axial forces generated during operation cancel each other out, completely abandoning the balance disc or balance drum devices relied upon by traditional multistage pumps. This design solves problems such as efficiency decline, axial vibration, and rotor seizure caused by balance disc wear in traditional pumps, increasing fault-free operation time to more than three times that of ordinary pumps.
2. High efficiency and energy-saving features
By removing the balance disc, it avoids the backflow loss of balance water (accounting for 5%-14% of traditional pump energy consumption) and disc friction loss, improving pump efficiency by an average of 3%-12%. In a real case, a coal mine in Jinzhong, Shanxi, saved 3% electricity year-on-year after using self-balancing pumps, significantly reducing annual operating costs.

[For more information on self-balancing multistage pump models, parameters, selection, and quotation plans, please click the image above]
-
Strong adaptability of self-balancing pumps: capable of handling complex mining conditions
Wear-resistant and corrosion-resistant flow parts use materials such as high-chromium alloy and wear-resistant cast iron, capable of conveying mine water, sewage, and corrosive media containing solid particles (≤1.5%, particle size ≤1.3mm), with an applicable temperature range of **-20℃~80℃**. For example, the MDP pump's impeller life is six times longer than traditional pumps when conveying mine slurry water.
High pressure and long-distance delivery performance: multistage boosting technology (single-stage lift up to 67m, total lift up to 1800m) meets deep well drainage and cross-regional water transfer needs. A certain open-pit mining project in Lianyungang used the ZPD720-60×3(P) pump, with a single pump daily drainage volume exceeding design requirements by 20%, successfully coping with peak drainage challenges during heavy rain.
-
High cost-performance ratio of self-balancing pumps: significant economic benefits
Reduced maintenance costs
Without vulnerable balance disc structure, annual maintenance frequency is reduced by 70%; modular design shortens the time to replace seals and bearings by 50%, with operation and maintenance costs only one-third of traditional pumps. For example, a coal mine's annual maintenance cost dropped from 1.2 million yuan to 400,000 yuan.
Extended service life
Precision casting technology and rigid shaft design (40Cr material) extend pump body life to 8-10 years, 3-6 times that of ordinary pumps.
-
Intelligent features: compatible with intelligent software
The intelligent monitoring system is equipped with real-time pressure, temperature, and vibration sensors, capable of remote fault warning and automatic speed adjustment to avoid downtime accidents. For example, Zhonglian Pump's intelligent pumps in the petrochemical industry reduce fault response time by 90%. Safety and compliance: the entire series has passed MT/T114-2005 mining safety certification and Coal Safety Mark (MA certification), and explosion-proof motors (YB3 series) meet underground operation requirements. Zhonglian Pump's self-balancing pumps have also obtained drinking water hygiene safety certification, expanding into municipal water supply fields.
5. Globalization trend
International recognition cases: global projects such as the Siberian mining area in Russia and the Shenmu coal mine in Shaanxi have adopted self-balancing pumps to replace traditional equipment, reducing failure rates by 80%. Zhonglian Pump's MSD pumps achieve stable operation at 300 bar high pressure in thermal power plants, becoming an industry benchmark. Future technology direction: the self-balancing structure is regarded as the "ultimate solution" for multistage pumps. Companies like Zhonglian Pump continue to optimize hydraulic models (CFD flow field analysis) and launch derivative models such as dual-inlet pumps (MDSP type), expanding flow range to 1350 m³/h to cover more industrial scenarios.
Self-balancing mining multistage pumps Through three core innovations—structural innovation (no balance disc), material upgrade (wear-resistant alloy), and intelligent control—it solves the pain points of traditional pumps such as low efficiency, frequent failures, and high costs. Its comprehensive advantages in energy saving (3%-14%), stability (vibration reduced by 80%), and long service life (6 times that of ordinary pumps) create economic value far exceeding initial investment costs throughout the entire lifecycle. With the rise of mining intelligence and environmental requirements, self-balancing technology will become an irreversible trend in the multistage pump field.
Latest News
Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha