-
Products
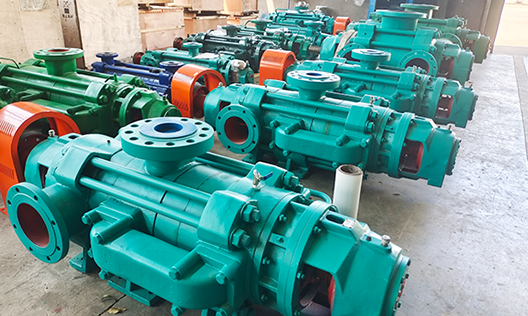
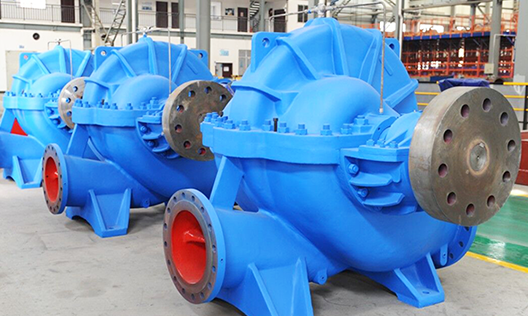
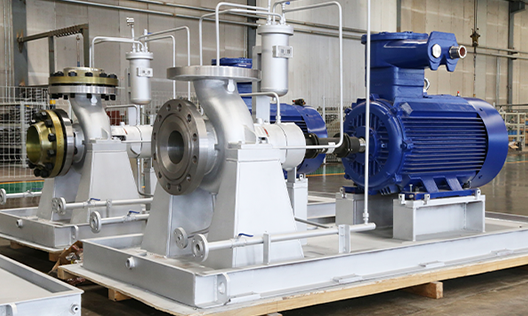
Puede fabricar 26 series de productos, incluyendo bombas de circulación para grandes centrales eléctricas, bombas de condensación para grandes centrales eléctricas, bombas petroquímicas, bombas multietapa, bombas de aguas residuales y lodo, bombas multietapa autoequilibradas, bombas de doble succión y única etapa tipo split, y bombas centrífugas de succión simple y única etapa.
-
Cases
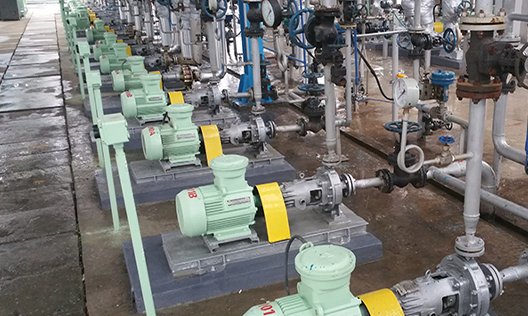
La elección de más de cientos de miles de clientes, cubriendo industrias como minería de carbón, metalurgia, química, energía, recursos hídricos, alimentos, municipalidades y protección ambiental, y exportando a Asia Sudeste, África, América y otros lugares.
-
Service
La empresa fue la primera en la industria en obtener las certificaciones internacionales del sistema de calidad ISO 9001:2008, del sistema de gestión ambiental ISO 14001 y del sistema de gestión de seguridad y salud ocupacional GB/T 28001, además de la certificación API 610 de la Asociación Estadounidense del Petróleo.
-
About us
La empresa, fundada en 1989, es una empresa nacional de alta tecnología integral que integra diseño, investigación y desarrollo, fabricación y servicios; actualmente es una empresa clave en la industria china de bombas centrífugas y una de las grandes fábricas especializadas.
-
Blogs
Con productos innovadores, calidad excepcional y servicios integrales, buscamos la verdad y la pragmática, avanzamos con iniciativa, y nos esforzamos por lograr el objetivo de ser "la marca líder en el campo de aplicación de bombas centrífugas en el país"! Raigada en Hunan, orientada a todo el país y hacia el mundo!
Mining high-pressure pump
Publication Date:
2025-09-05
Author:
Source:


The mining high-pressure pump is a flagship pump type specifically designed for mine drainage, tunnel construction, and urban flood prevention—critical applications in the mining industry. It is an efficient and reliable piece of industrial equipment. Given that these pumps often operate in challenging environments with complex water inflows, as well as meeting demanding requirements for high head and large flow rates, mining high-pressure pumps typically feature a multi-stage design.
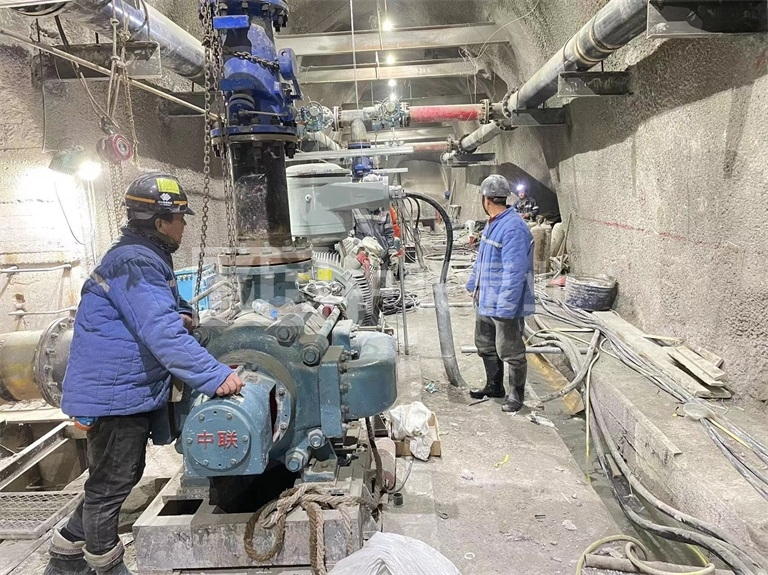
The main features of mining high-pressure pumps include high pressure and large flow rates, along with characteristics such as high efficiency, reliability, safety, and cost-effectiveness. These pumps are primarily composed of a motor, pump body, control cabinet, and a remote intelligent control system, enabling them to swiftly lift water or other liquids from deep underground to the surface. Additionally, high-pressure pumps boast wear resistance, corrosion resistance, durability, and an extended service life, making them well-suited to meet diverse drainage requirements in various applications.
Common types of high-pressure pumps for mining:
1. Multistage centrifugal pump : Multistage centrifugal pump Featuring high flow rate, high head, exceptional efficiency, and low noise levels, these pumps are among the top choices for drainage applications in mining, large-scale engineering projects, and other industries. Currently, there are only a few brands on the market that hold both Coal Safety Certification and Mining Safety Certification, primarily based in Changsha, Hunan Province. Notable brands include Zoomlion Pump Industry, SanChang Pump Industry, and Canon Pump Industry. Among them, Zoomlion Pump Industry offers a comprehensive lineup of over 2,000 models—covering various specifications—featuring multi-stage centrifugal pumps certified for mining and coal safety. These products are widely distributed across 28 provinces in China, as well as in several countries and regions in Africa and Southeast Asia. With extensive industry experience, Zoomlion’s pumps are renowned for their outstanding wear resistance and superior performance, making them an excellent choice for high-pressure drainage applications in the mining sector.

↑Click the image to learn more about Zhonglian Pump Industry's [Mining Multistage Centrifugal Pump]—view product details and parameter information here↑
2. Self-balanced multistage pump : Self-balanced multistage pump This is a new type of multistage centrifugal pump designed based on the principle of multi-stage centrifugal pumps, featuring a left-right symmetrical impeller arrangement and incorporating technologies such as a throttling sleeve in the middle section to achieve self-balancing of axial forces. The pump boasts a compact internal structure, occupies minimal floor space, operates with low noise levels, and exhibits exceptional durability. Currently, there are only a few brands of wear-resistant, self-balancing centrifugal water pumps for mining applications available on the market, primarily concentrated in Changsha, Hunan Province. Prominent brands include Zhonglian Pump Industry, SanChang Pump Industry, and Canon Pump Industry. Among them, Zhonglian Pump Industry offers a comprehensive range of models—over 2,000 specifications—including those certified for Mine Safety and Coal Safety. Their self-balancing multistage pumps are sold across more than 20 provinces nationwide, as well as in several countries and regions in Africa and Southeast Asia. With extensive industry experience, these pumps are renowned for their outstanding wear resistance and superior performance, making them an excellent choice for high-pressure drainage applications in mining environments. The product line has now been optimized and upgraded to the 13th generation, earning widespread recognition within the industry.

In short, Multistage centrifugal pump Self-balancing multistage pumps are one of the commonly used pump types in fields such as mining and large-scale engineering projects. The key difference is that self-balancing multistage pumps incorporate self-balancing technology, resulting in higher operational efficiency and improved durability. Selection and configuration should be tailored to meet specific drainage and engineering requirements.
Previous:
Recommended Information


Related Products
Perhaps you also want to know?
Zoomlian Pump Industry
Address:No. 210, Environmental Protection Middle Road, Yuhua Economic Development Zone, Changsha City, Hunan Province China
All rights reserved © Changsha Zoomlian Pump Co., Ltd.
This website supports IPv4 IPv6 bidirectional access
Website construction:Zhongqi Power Changsha